The next generation of our innovative belt hoist has arrived. Konecranes Belt Hoist 2 is now rated for both technical cleanliness and cleanroom applications.
We have extensive experience in hoist design for applications requiring technical cleanliness, and now, cleanrooms as well. The Konecranes belt hoist got a major upgrade to deliver even more options for its use in a wide variety of industrial settings.
A complete product redesign and brand-new certification that opens the door for use in cleanrooms through level 7, brings new options for applications that require technical cleanliness or cleanrooms to operate.
Technical cleanliness certifications regulate levels of contamination allowed on surfaces, while cleanroom certification levels, much more stringent, regulate contaminants in the air. Our belt hoist was originally developed for use in the French cheese industry. Its patented non-metallic belt design made of Dyneema® removed the need for lubrication, a possible source of contamination, and its composition eliminated the possibility of metal fragments falling into the product.
High-strength polyamide pulleys support the belt, which is resistant to acids, bases, mineral salts, solvents and oil. With IP55 shielding and an electrically isolated hook block, the belt hoist maximizes safety wherever you use it. Easy to install on different kinds of lifting systems such as overhead traveling cranes, Konecranes KBK workstation lifting systems, jib cranes, monorails and stationery applications, the hoist can support up to 6.3 tons.
Proven over decades
Thirty years ago, the Konecranes belt hoist was a game changer in the food industry, and over the past three decades it also found a home in other niche markets where extreme cleanliness, or “technical cleanliness,” according to ISO EN 16232, is a primary requirement. Currently, its largest market is semiconductor manufacturing, but many other industries that demand the highest level of cleanliness have also lined up to incorporate this hoist into their manufacturing processes. These include electronics, optics, aerospace, pharmaceutical and biotechnology, as well as the automotive industry’s push into electric vehicles.
During this same time period, we continued to innovate our hoists for other uses, developing technologies to improve motors, gearing, voltage range and incorporate inverter control for stepless traveling and lifting. This non-stop product evolution has helped cement our reputation as a global lifting leader and expand our worldwide customer base.
What’s new in the Konecranes Belt Hoist 2?
Fast-forward to today, where many of these lifting technologies developed for other in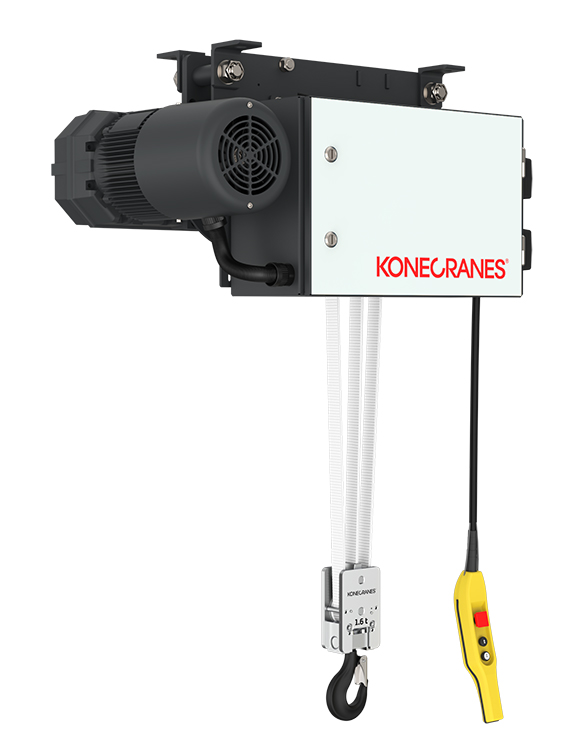 dustries have now been integrated into the Belt Hoist 2, preserving and enhancing its extreme clean-use capability while improving maintainability and lifting precision.
The new, modern motor doubles the duty range, delivering 60% ED instead of 30% ED, with a closed, lifetime maintenance-free brake design and motor/gear coupling to enhance clean operation. The protection class of Belt Hoist 2 motors is now IP66 as a default, offering substantially better protection against dust than the earlier IP54 standard.
In addition, requests from customers led us to develop an extended load range for lower capacity loads, which, combined with inverter controls, delivers maximum flexibility for more applications. The new range offers 125 kg and 250 kg hoists in addition to the original 500 kg model, along with a number of hoist configurations that accommodate low-headroom requirements and include multiple suspension options to maximize workspace.
Certified for cleanroom use by the Fraunhofer Institute
The Konecranes Belt Hoist 2 is among the few hoists certified for cleanroom use by the Fraunhofer Institute for Manufacturing, Engineering and Automation IPA, in compliance with cleanroom standards ISO14644-1 and -14. The Belt Hoist 2 has been tested with various setups and certified with and without loads, and also with motor trolley, for level 7. Level 6 certification is our next target for this versatile hoist.
Material upgrades that have made this evolution possible include stainless steel wheels, a stainless-steel hook block and hook, and beams and runways also formulated from stainless steel. Cleanroom applications typically prohibit copper, zinc and nickel, particularly with semiconductor production. Also, lubricants and paint must be silicone-free.
With the launch of the Belt Hoist 2, we continue to expand our offering of hoists for cleanrooms and applications requiring technical cleanliness. Even though the original belt hoist was already a winner with customers for technical cleanliness, expanding into cleanroom use has been a persistent goal worthy of the most-evolved materials and technologies available. The Konecranes Belt Hoist 2, now with cleanroom certification through Level 7, addresses key customer requirements: increased cleanliness, robustness, better maintainability and lower manufacturing costs.
Learn more about Konecranes belt hoist
Learn more
